MES, Inc.
RESILIENT

Energy Storage & Backup Power

Cabinet, busbar and enclosure hardware for grid-scale storage and data center standby.

MES extrudes, casts, machines and forges the metal components inside battery energy storage and standby power equipment — in eight countries, with our own engineers on the floor.

What Changed

5 Pressures on Storage & Standby

Five pressures on storage and standby sourcing that were not there three years ago.

01

Data center ride-through

Every hyperscale facility needs batteries to bridge to generator start, and increasingly a larger BESS for peak shaving.

02

Air to liquid

Air-cooled cabinets are giving way to liquid, because temperature uniformity across a module stack sets degradation rate. That moves thermal content from sheet metal to machined and die cast plates.

03

Domestic content rules

Storage projects frequently carry domestic content requirements tied to tax credit qualification.

04

Copper cost basis

Since April 2026, Section 232 duty on covered copper is assessed on full customs value. A single cabinet contains 200 to 600 machined and plated interconnect joints.

05

Twenty-year outdoor life

These enclosures sit in coastal and desert environments for two decades. Alloy and finish have to be specified together.

Applications

Four Applications. One Enclosure Capability.

Storage and standby power serve the data center and the grid. The purposes differ. The mechanical content is close to identical — large outdoor-rated enclosures, structural framing, current-carrying busbar and thermal plates.
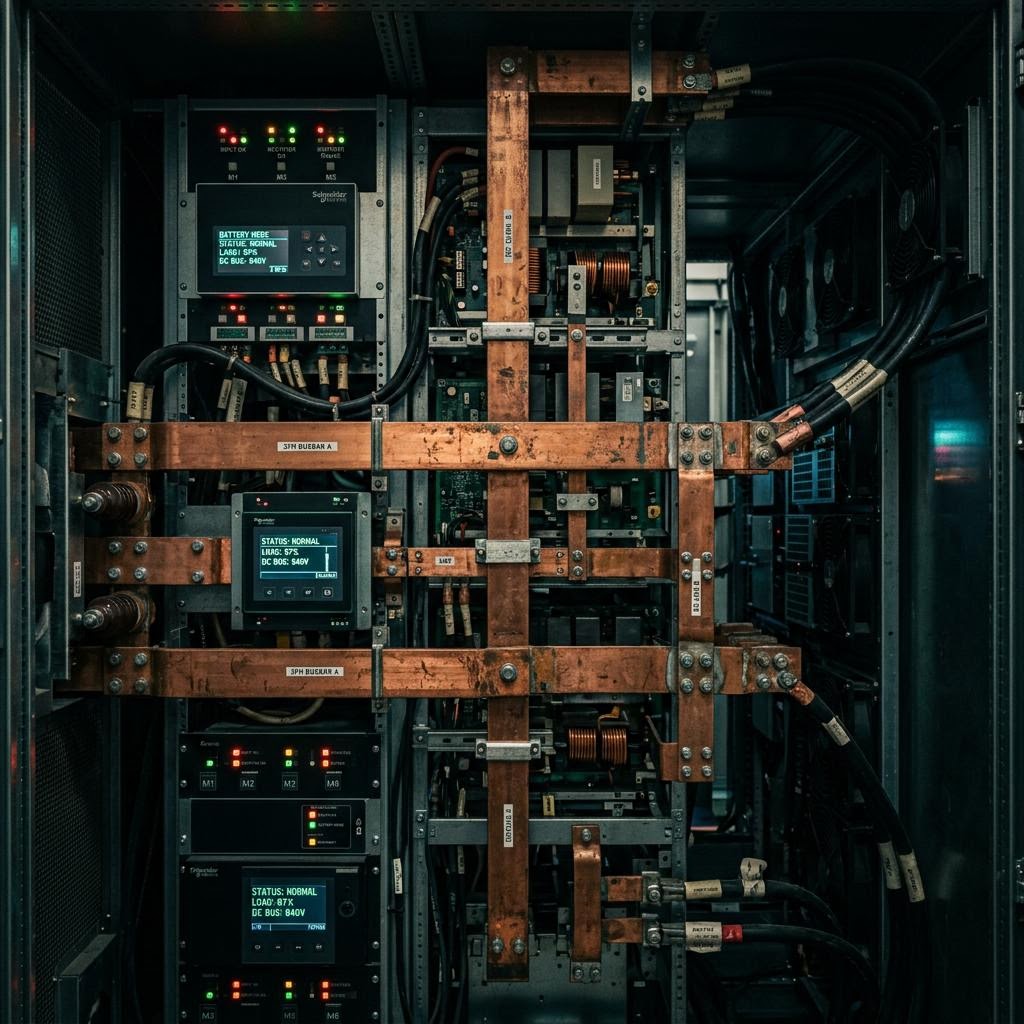
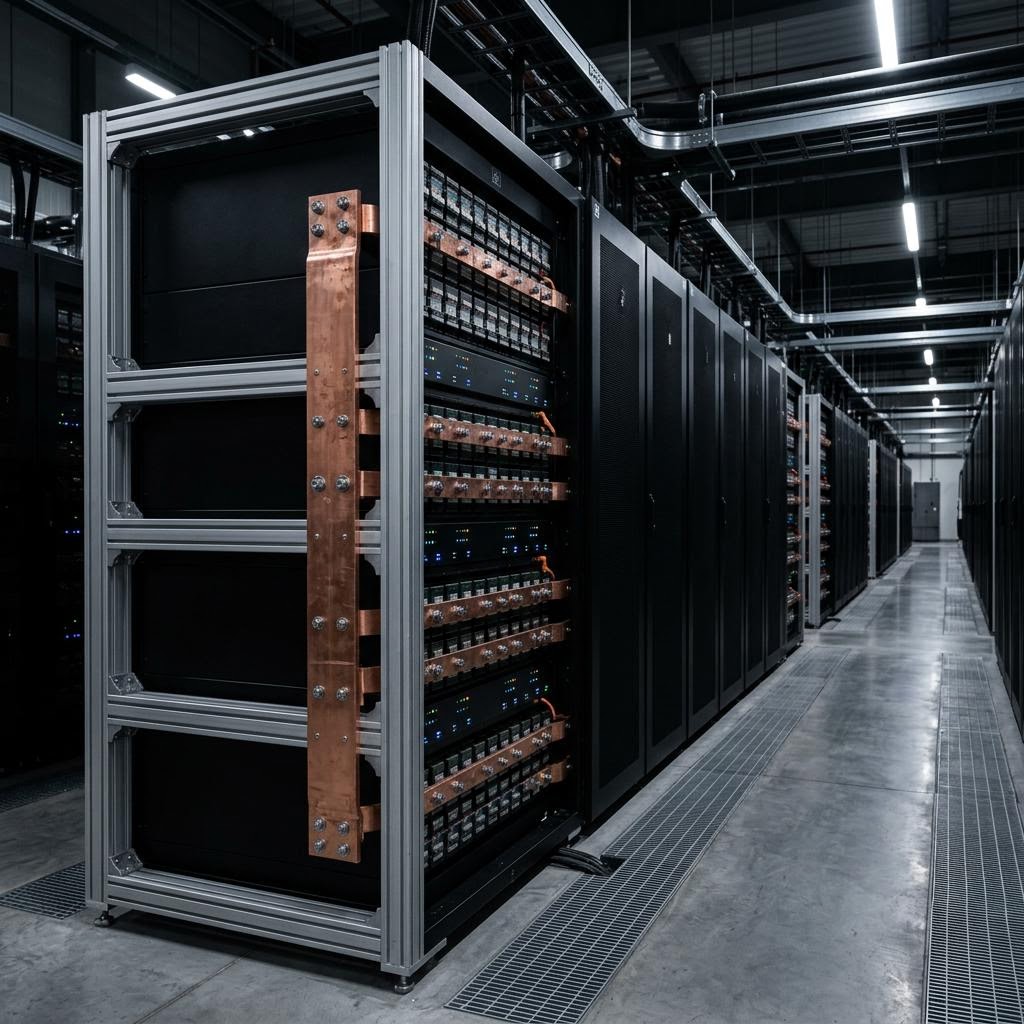
DATA CENTER RIDE-THROUGH & STANDBY
01

DATA CENTER RIDE-THROUGH & STANDBY

Batteries bridge seconds to minutes. Generators carry anything longer.

Critical Spec

The spec that matters: joint integrity across 200 to 600 bolted connections in a thermally cycling cabinet.

Materials

6005A-T6 · A380 aluminum · C11000 copper · 316 stainless · CF8M · 310S

Typical Supply Chain

Vertiv · EnerSys · Caterpillar · Cummins · Generac · Rolls-Royce mtu · Kohler · Bloom Energy
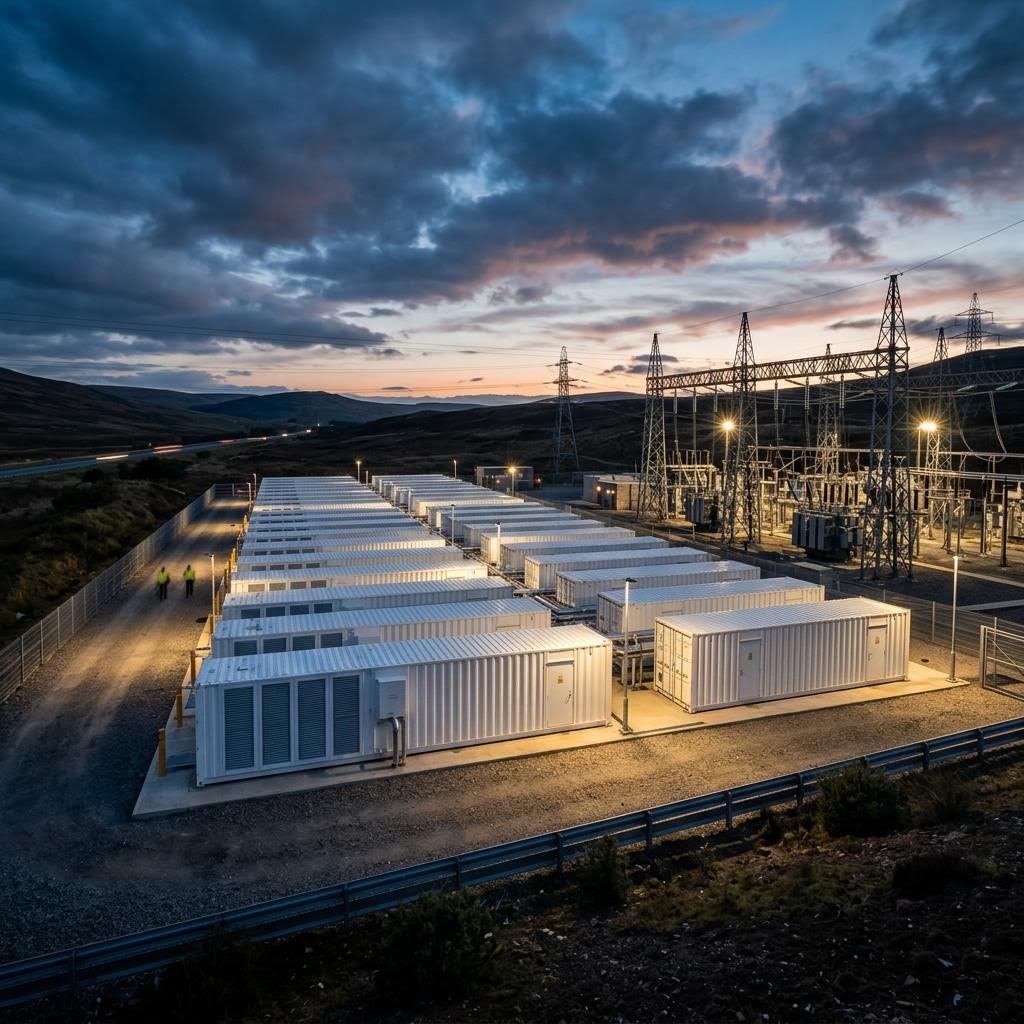
GRID-SCALE BATTERY STORAGE
02

GRID-SCALE BATTERY STORAGE

Four-hour and longer duration, cycling daily rather than rarely.

Critical Spec

The spec that matters: 5 mm minimum wall in a compression-loaded end plate, ASTM E505 Level 2 porosity.

Materials

6005A-T6 · 6063-T6 · A380 aluminum · C11000 copper · 316 stainless

Typical Supply Chain

Fluence · Tesla Energy · Powin · Wärtsilä · LG Energy Solution · Samsung SDI · CATL
POWER CONVERSION & INVERTERS
03

POWER CONVERSION & INVERTERS

The equipment between the battery and the grid. Several percent of throughput rejected as heat.

Critical Spec

The spec that matters: 0.05 mm flatness and 0.8 µm Ra under the power module.

Materials

6063-T6 · 6061-T6 · C11000 copper · A380 aluminum

Typical Supply Chain

Sungrow · EPC Power · Dynapower · SMA America · Ingeteam · Advanced Energy · TMEIC
STANDBY GENERATION
04

STANDBY GENERATION

Diesel, gas and emerging fuel cells. Ancillary and enclosure content, not engines or hot-section parts.

Critical Spec

The spec that matters: high-mix, low-volume against a rigid engine interface — 250 to 5,000 pieces a year, certified.

Materials

6063-T6 · 6005A-T6 · A380 aluminum · CF8M · 310S · Inconel-family

Typical Supply Chain

Caterpillar · Cummins · Generac · Rolls-Royce mtu · Kohler Power · Bloom Energy
Data center infrastructure
SEE IT RUNNING

The Parts Behind Data Center Power

Batteries bridge the seconds. Generators carry the hours. Every enclosure, busbar and bracket in between is a part somebody had to machine, cast or extrude.

Why MES

Why Storage & Standby Manufacturers Work With MES

Because a battery cabinet fails in ways that pass a first article. Porosity in a compression-loaded end plate reduces effective wall section without changing anything measurable from outside the part. Fifty microhms of resistance rise per joint is invisible on one connection and significant across four hundred.

We review the drawing before the tool is cut. We measure every lot at source.

Certified & Global

  • ISO 9001:2015 since 2009
  • IATF 16949
  • NMSDC Minority-Certified
  • Eight countries

WE REVIEW THE WALL SECTION FIRST

A die cast end plate holds a cell stack at preload for twenty years. We specify 5 mm minimum wall in the loaded region and review gating before the first shot.

WE MEASURE AT SOURCE, EVERY LOT

Cooling plate flatness to 0.10 mm against the module face, verified in the supplier's plant. First article on 100% of features, then 5 pieces per lot.

WE SPECIFY FINISH WITH THE ALLOY

1,000 hours salt spray coastal, 500 inland — including at machined faces and cut ends, which is where corrosion starts.

WE EMPLOY THE ENGINEERS IN THE PLANT

Same country, same floor, the day your parts run. Not a quarterly audit the factory prepared for.

Capability Limits

Size, Tolerance and Volume Ranges

What we hold and where the limits are.
Cabinet, container and structure

01

Cabinet, Container
& Structure

1.5 mm
Extrusion min wall on 6005A structural
up to
2,400 mm
Welded cabinet height frame squareness ±1.5 mm
Salt spray, coastal 1,000 hours minimum · Type II anodize 15 to 25 µm
Container footprint up to 6 m · ISO framing
Extruded profile circle up to 300 mm circumscribing
Extruded length up to 6 m · precision straightened to 0.5 mm/m
Extrusion wall, general 1.2 mm on 6063
Salt spray, inland spec 500 hours minimum
Cast, machined and forged limits

02

Cast, Machined
& Forged

5 mm
Load-bearing wall minimum in compression regions
0.10 mm
Cooling plate flatness against the module face
Busbar tin plating 5 to 15 µm · at the joint face
High-temp service up to 850 °C · 310S & Inconel-family
Die casting size 5 g to 40 kg · 50 to 4,400 ton presses
Die cast wall, general 1.5 mm minimum aluminum · 0.8 mm zinc
Module end plate porosity ASTM E505 Level 2 max in loaded areas
Cooling plate size up to 400 × 900 mm
Interconnect busbar 3 to 16 mm thick · 20 to 150 mm wide
Investment casting 10 g to 50 kg · ±0.13 mm on first 25 mm
Annual volume 250 to 100,000 pieces per part number
Quality

How We Prove It Before It Ships

Every number on the drawing has to be measured by someone, somewhere. We do it in the supplier's plant, on the parts that ship — not on your dock, and not on a first article that was made under conditions the production run will never see.

A die cast end plate holds a cell stack at preload for twenty years. It fails from the inside, and nothing about the failure is measurable from outside the part. Four checks catch it before the container leaves.

ASTM E505 Level 2 max Porosity in load-bearing walls

A cast wall with internal voids has less effective section than the drawing says. The part measures correct, weighs close to correct, and yields early under sustained load. Level 2 is the acceptance limit we hold in loaded regions — looser elsewhere, because porosity in a non-structural boss costs nothing.

Ultrasonic thickness Wall verification 5 pieces per lot in loaded regions

Wall thickness in a die casting drifts as the tool wears and as thermal balance shifts across a shift. We measure it ultrasonically rather than by section-and-inspect, because destructive testing tells you about the part you destroyed.

Before the first shot Gating review not after the first field return

Porosity is a gating and thermal problem, not an inspection problem. It gets designed in or designed out at the tooling stage. We review gate location, wall transitions and cooling before the tool is cut — which is the only point where fixing it is cheap.

Available on request Compression testing for end plate qualification

Where a customer needs preload performance proven rather than inferred, we can test to the specified load. Most programs do not need this. The ones that do are usually first-of-kind designs where the wall section is being pushed.

XRF at the joint face Plating thickness per lot, not on the flat
ASTM B571 Plating adhesion bend or tape test, per lot
1.5× working pressure Cooling plate leak test pressure decay, 60 second hold, 100%
ISO 16232 Cleanliness flush and filter verification
ASTM B117 Salt spray 500 or 1,000 hours per specification
Machined faces & cut ends Coating thickness measured where corrosion starts
100% of features First article AS9102 format
PPAP Level 3 standard Documentation Level 4 available · 10 year retention
Timeline

Standard Lead Times

The journey from quote to shipped parts. Fast-path engineering and stock deliveries move in days; hard tooling moves in weeks — and with stock in Columbus, Monterrey and Poland, a qualified part is two to five days from your dock rather than thirty days from a port.

Step 01

3 to 5 business days

Quote turnaround

Step 02

5 business days

DFM feedback

before tooling · no cost

Step 03

3 to 5 weeks

Prototype, fabricated frame

Step 04

6 to 10 weeks

Extrusion die

Step 05

10 to 18 weeks

Die casting tool

Step 06

2 to 4 weeks

First article inspection

from tool approval

Step 07

8 to 12 weeks

Production, tooled part

Step 08

2 to 5 days

From stock

from Columbus, Monterrey or Poland

Components

Components We Engineer & Deliver

Four assemblies. Aluminum extrusion, high-pressure die casting, precision CNC machining, investment casting and forging.

The structure, and the parts holding cell modules under compression for twenty years.

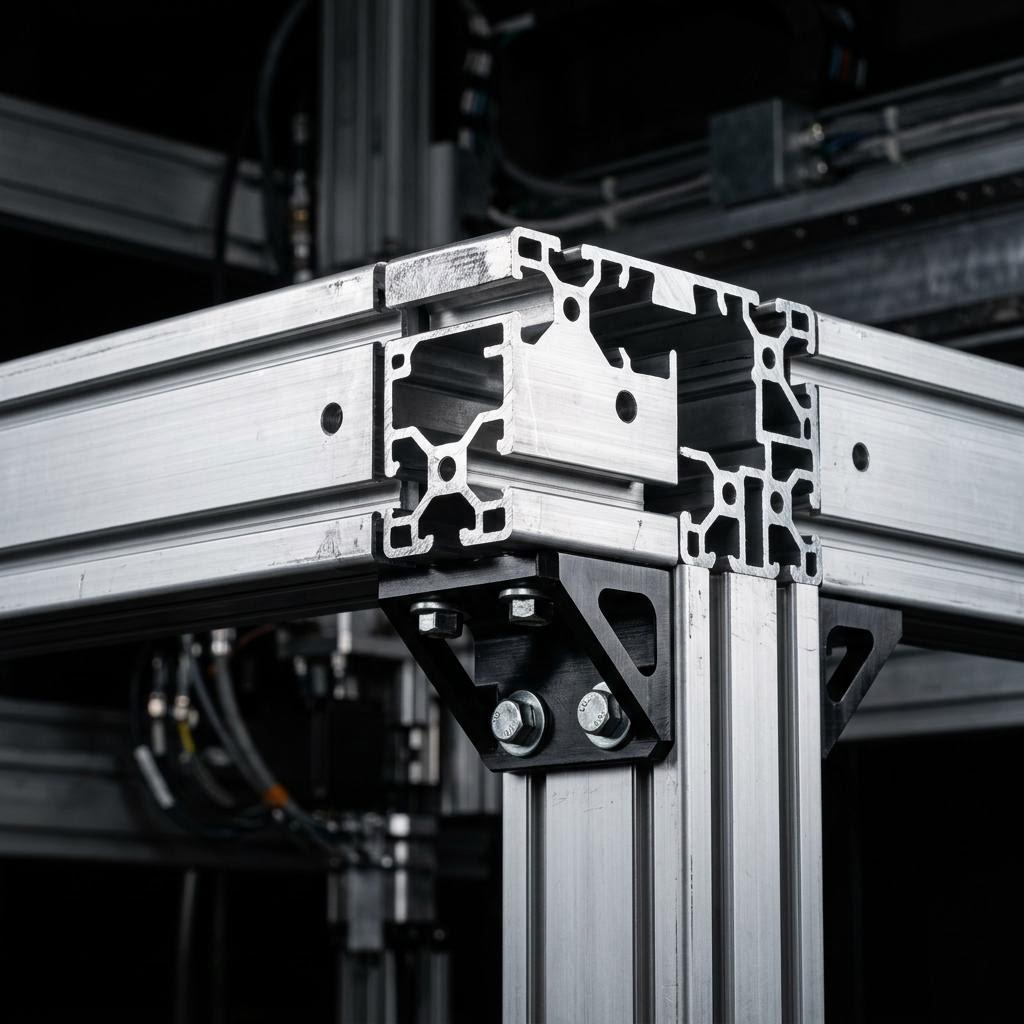
Cabinet and container frame extruded and welded 6005A-T6 to 2,400 mm, ±1.5 mm squareness
Module tray cast and extruded aluminum, 1.5 mm minimum wall
Module end plate A380 die cast — 5 mm minimum wall in the loaded region
Compression tie rods and hardware forged and machined, certified per heat
Base frame and skid structural extrusion and casting
Leveling feet and seismic anchors machined and forged
Door, hinge and latch hardware zinc die cast, 10,000 cycle, 1,000 hr salt spray
Cable gland and entry plates machined aluminum

200 to 600 bolted joints per cabinet, each one a potential resistance rise. And a thermal system moving from air to liquid.

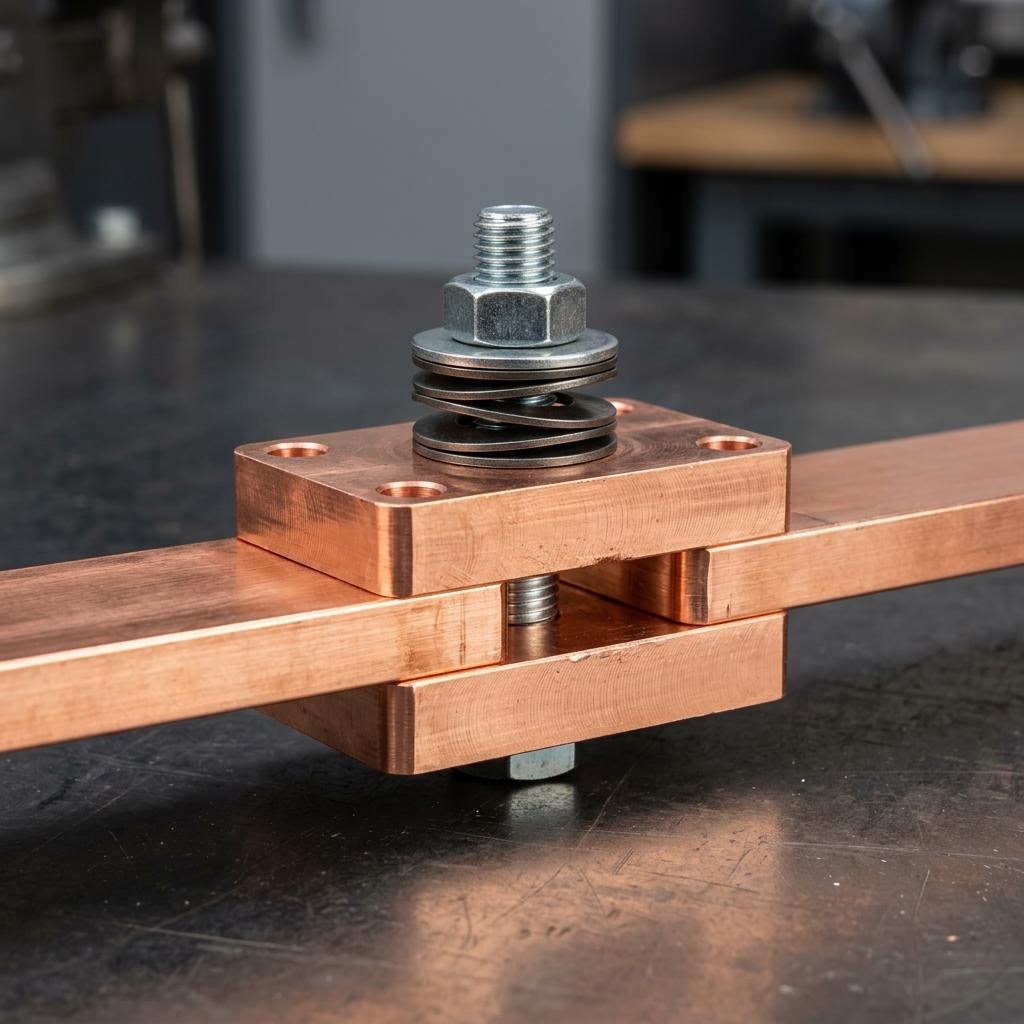
Interconnect busbar machined C11000, tin plated 5 to 15 µm at the joint face
Terminal landing block machined copper, 100% IACS
Module-to-module flexible links machined and formed copper
Ground bus and bonding hardware machined copper
Cooling plate die cast then machined to 0.10 mm flatness, up to 400 × 900 mm
Coolant manifold and headers extruded and machined, pressure tested 100%
Quick-disconnect and port bodies machined brass or 316
Fan shrouds and housings A380 die cast, 1.5 mm minimum wall

Inverters and PCS between the battery and the grid. The heat sink base under the power module is the critical interface.

IGBT and module heat sink base extruded then machined to 0.05 mm flatness, 0.8 µm Ra
Enclosure frame and panels extruded and machined aluminum
DC and AC busbar machined C11000, plated — 3 to 16 mm thick
Filter inductor and capacitor brackets stamped, cast and machined
Cable gland plate machined aluminum
Cooling fan brackets and shrouds die cast and stamped

Ancillary and enclosure content around the engine. High-mix, low-volume, against a rigid interface.

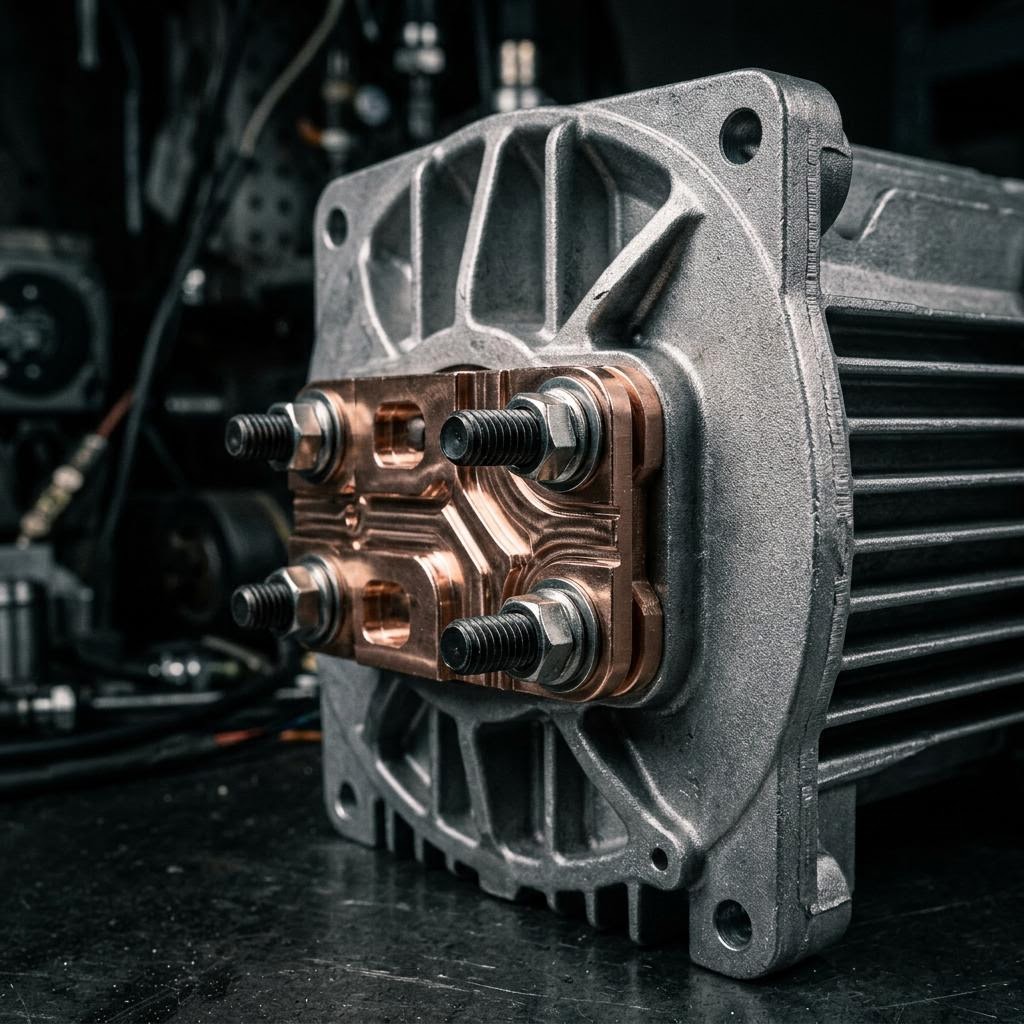
Alternator end bracket cast and machined, ±0.05 mm on bearing seats
Engine mounting bracket and isolator plate cast and machined
Exhaust manifold flange investment cast CF8M or 310S, service to 850 °C
Turbocharger mounting bracket investment cast and machined
Canopy and acoustic enclosure framing 6063 and 6005A extrusion
Radiator coil frame and end plates extruded and machined
Fan shroud A380 die cast
Lifting lugs and base rails forged, 4:1 design factor, certified per heat
Engineering

What Engineers Ask Us

Five specifications decide whether a storage cabinet performs for twenty years outdoors. All five are set on the drawing.

01WALL SECTION: SPECIFY IT WHERE THE LOAD IS

A die cast end plate holds a cell stack at preload for twenty years.

Porosity in a load-bearing wall reduces effective section without changing anything measurable from outside the part. Specify 5 mm minimum wall in the loaded region, ASTM E505 Level 2 maximum porosity, and ultrasonic thickness verification per lot. Require a gating review before the first shot.

02INTERCONNECT PLATING: A NUMBER, NOT A NOTE

A cabinet contains 200 to 600 joints, each conducting through its plating.

Fifty microhms of resistance rise per joint is insignificant on one connection and material across four hundred. Specify tin at 5 to 15 µm, the governing standard, and that it is measured at the joint face by XRF rather than on the flat.

03COOLING PLATE FLATNESS: AGAINST THE MODULE FACE

Uneven contact means uneven cell temperature means uneven degradation.

A die cast plate dimensionally correct across its outline can still be dished 0.3 mm across the contact area. Cells at the hot end of a stack degrade faster, and the weakest cells set module capacity. Specify 0.10 mm flatness against the module face, separately from the general profile tolerance.

04OUTDOOR FINISH: SPECIFY IT WITH THE ALLOY

Corrosion starts at machined faces and cut ends.

A 6005A extrusion coastal needs a different system than the same part inland — 1,000 hours salt spray per ASTM B117 against 500. Specify the hours, the coating system and the alloy as one requirement, and state what happens at machined faces. Coastal and agricultural sites justify 316 fasteners over 304.

05GENERATOR ANCILLARIES: NAME THE ENGINE INTERFACE

An exhaust flange matches a specific engine, not a general spec.

Alternator end brackets match a frame size and need ±0.05 mm on bearing seats. Neither has enough annual volume — typically 250 to 5,000 pieces — to interest a shop wanting long runs. Specify the mating interface and the certification requirement together, and expect qualification to take longer than the part suggests.

200 to 600
Bolted Joints

Bolted interconnect connections in a single battery cabinet.

20 Years
Outdoor Service Life

1,000 hours salt spray coastal.

Boundaries

Where We Are Not the Right Answer

The fastest way to be believed about what we can do is to be specific about what we cannot.

  • Domestic melt and pour. Storage projects with tax-credit domestic content requirements often need it. If yours does, we will say so and point you toward a domestic source.
  • Cells, battery management systems and fire suppression. OEM-supplied — not our lane.
  • Engines, alternators and hot-section turbine components. We supply the ancillary and enclosure content around them.
  • ITAR-controlled work and DFARS specialty metal restrictions.
  • NQA-1 nuclear programs.
  • Volumes under 250 pieces a year on a hard-tooled part.
Capabilities

Five Processes. One Partner.

Processes

01

Aluminum Extrusion

Cabinet and container framing, module trays, coolant headers, canopy framing. To 300 mm circumscribing circle, 6 m lengths, 1.5 mm minimum wall on 6005A, straightened 0.5 mm/m.

02

High-Pressure Die Casting

Module end plates, cooling plates, DC disconnect enclosures, fan shrouds. 50 to 4,400 tons, 5 g to 40 kg, 5 mm minimum wall in load-bearing regions.

03

CNC Machining

Interconnect busbar, terminal blocks, cooling plate faces, heat sink bases. ±0.05 mm general, ±0.013 mm critical, 0.10 mm flatness on plate faces.

04

Investment Casting

Exhaust manifold flanges, turbocharger brackets. 10 g to 50 kg in CF8M, 310S and Inconel-family, service to 850 °C.

05

Forging

Compression tie rods, lifting lugs, seismic anchors. 50 to 4,400 tons, 4:1 design factor, certified per heat lot.

Materials

6005A-T6 and 6063-T6 aluminum

6005A where framing carries structural and seismic load · 1.5 mm minimum wall · 6063 for panels and trays at 1.2 mm

A380 aluminum

Module end plates, cooling plates, enclosures · 1.5 mm general and 5 mm load-bearing minimum wall · ASTM E505 Level 2 porosity

C11000 copper

Interconnect busbar and terminal blocks · 100% IACS · 3 to 16 mm thick · Tin plated 5 to 15 µm at the joint

316 and CF8M stainless

Fasteners and fittings coastal where 304 is insufficient · CF8M for investment cast wetted components

310S and Inconel-family alloys

Exhaust-side generator components in service to 850 °C

FAQS

FREQUENTLY ASKED QUESTIONS

Let's Build the Storage and Standby Layer

Scaling BESS cabinet production, moving a thermal design from air to liquid, or consolidating generator enclosure content into one supplier — MES delivers the components and the supply chain to get there faster.

BESS Integrator · Inverter and PCS OEM · Generator OEM · Data Center OEM