MES, Inc.
PROVEN

Transformers & Switchgear

The hardware around the electrical core — for the grid and for AI data centers.

MES machines, casts, forges and extrudes the metal components inside transformers and medium-voltage switchgear — in eight countries, with our own engineers on the floor.

What Changed

Five pressures on transformer and switchgear sourcing that were not there three years ago.

01

Replacement demand

A large share of North American distribution transformers are at or past design life. Structural demand on a decade-long timeline, not a cycle.

02

Data center load

Every hyperscale campus needs its own substation, unit substations and medium-voltage switchgear. A second demand curve on top of replacement.

03

Technician-hours, not material

Winding, core stacking and high-voltage testing take years to learn. Plant output is gated by labor, which makes an hour lost waiting on a bracket unrecoverable.

04

A thinning domestic supply base

Pace Industries closed plants in Arkansas, Michigan and Tennessee in one announcement. The shops that remain increasingly decline high-mix, low-volume hardware.

05

Copper cost basis

Since April 2026, Section 232 duty on covered copper is assessed on full customs value, not metal content.

Why Transformer & Switchgear Manufacturers Work With MES

Because the parts that stop a build are the ones nobody was watching. A twelve-dollar bracket gets a purchase order. A core assembly gets a sourcing manager and a quarterly review.

We supply the hardware around the core. Five processes, one relationship, one set of documentation.

01

WE PULL THE HEAT NUMBER AT THE MILL

Forged lifting lugs and anchor rods certified per heat, captured at the point of pour. Heat number on the packaging, records retained 10 years.

02

WE REVIEW THE DRAWING FIRST

A plating callout with no thickness. A radiator panel specified to standard bow. DFM feedback in 5 business days, before the tool is cut, at no cost.

03

WE PRESSURE TEST AT SOURCE

Relief valve bodies tested to 1.5× crack pressure on 100% of parts, in the supplier's plant, not on your dock.

04

WE EMPLOY THE ENGINEERS IN THE PLANT

Same country, same floor, the day your parts run. Not a quarterly audit the factory prepared for.

Certified & Global
ISO 9001:2015 since 2009 · IATF 16949 · NMSDC Minority-Certified · Eight countries · Supplying global power management manufacturers including Eaton
APPLICATIONS

Three Applications. One Component Portfolio.

Transformers and switchgear serve the utility grid and the AI build-out. The equipment is the same. The schedule is not — and that changes who will qualify a new supplier.

UTILITY GRID & DISTRIBUTION
01

UTILITY GRID & DISTRIBUTION

Replacement demand on a decade timeline. Standards documents that change slowly.

Components
Bushing wells · relief valves · lifting lugs · radiator sections · tap changer shafts · drain valves · cabinet hardware · ground pads
Materials
C11000 copper · C36000 brass · A380 aluminum · 6063-T5 · ASTM A668 Cl.D · Zamak 3/5
Critical spec
The spec that matters: heat-lot traceability on load-bearing forgings, with MT or UT per lot.

Prolec GE · ERMCO · Virginia Transformer · Howard Industries · Delta Star · Hitachi Energy
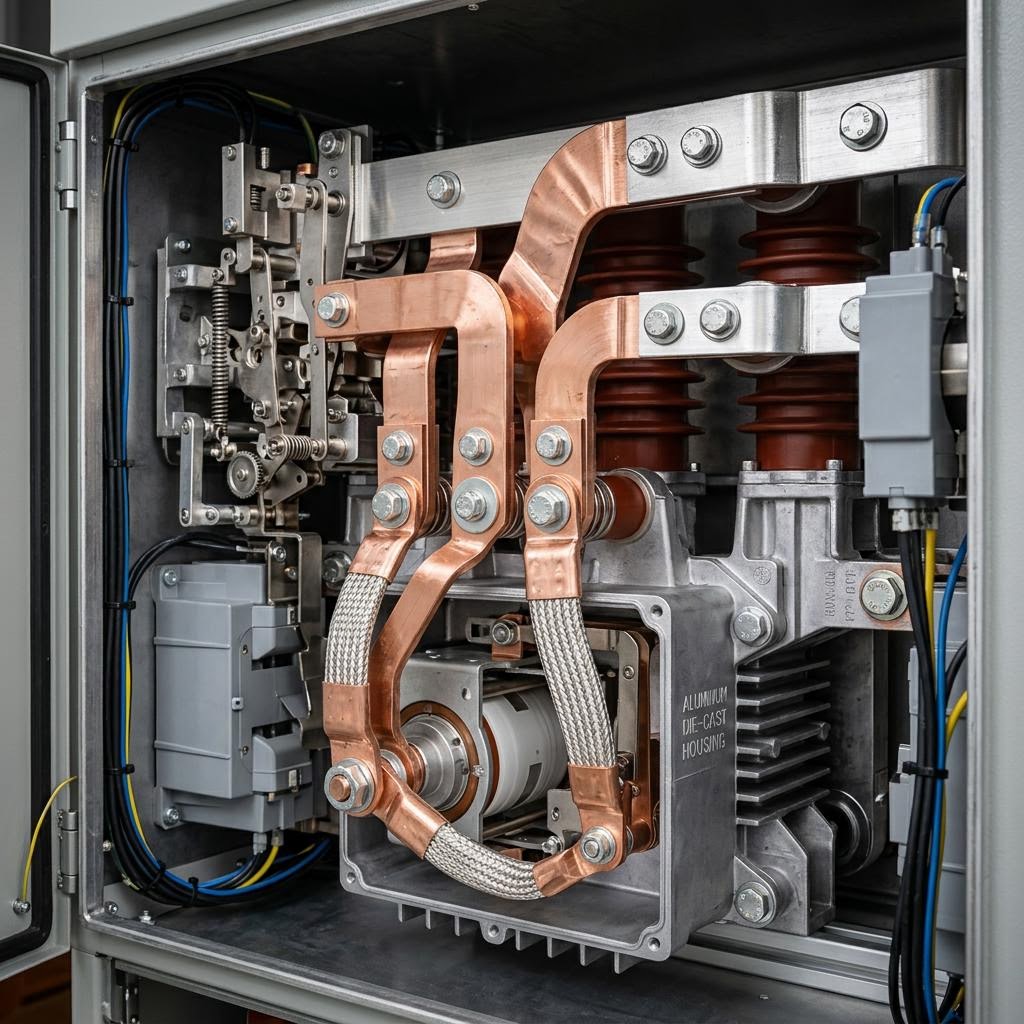
DATA CENTER POWER INFRASTRUCTURE
02

DATA CENTER POWER INFRASTRUCTURE

A hyperscale campus contains a compressed copy of the grid, built on a two-year schedule.

Components
Mechanism housings · primary bus and bus stabs · breaker cradles · trip latches · operating shafts · enclosure framing · cable entry plates
Materials
C11000 copper · A380 aluminum · 17-4PH H900 · 4140 Q&T · 6005A-T6 · 6063-T6
Critical spec
The spec that matters: ±0.05 mm bore-to-mounting-face on mechanism housings, across 10,000 operations.

Eaton · Schneider Electric · Siemens · ABB · Powell Industries · Myers Power Products

SUBSTATION & PROTECTION EQUIPMENT
03

SUBSTATION & PROTECTION EQUIPMENT

Reclosers, switches and protection gear between the transmission line and the load.

Components
Turret flanges · jacking lugs · oil valve bodies · lead clamps · insulator brackets · instrument transformer mounts
Materials
C11000 copper · CF8M stainless · A668 Cl.D forgings · A380 aluminum
Critical spec
The spec that matters: 0.10 mm flatness across a gasket face up to 1,200 mm in diameter.

S&C Electric · Hitachi Energy · Mitsubishi Electric · AZZ · G&W Electric

One portfolio, two schedules. A utility buys against a standards document through a framework agreement. A data center buys against an energization date with a signed lease behind it. The second will qualify a new supplier under pressure. The first usually will not.

CAPABILITY LIMITS

The Envelope

What we hold and where the limits are.

Bushing well diameter
25 mm to 75 mm
Bushing well weight
0.2 kg to 1.5 kg
Thread class
2A/2B standard · 3A/3B available
Plating, tin
8 to 20 µm at the contact face
Plating, silver
5 to 13 µm at the contact face
Turret flange diameter
up to 1,200 mm
Flatness, gasket face
0.10 mm across the sealing area
Surface finish, gasket face
1.6 µm Ra or better
Forged lifting lug
0.5 kg to 12 kg · 4:1 design factor
Forged shaft
Ø12 to Ø60 mm · to 900 mm · straightness 0.1 mm/100 mm
General machining tolerance
±0.05 mm · ±0.013 mm on critical features
Die casting
5 g to 40 kg · 50 to 4,400 ton presses
Die cast wall, minimum
1.5 mm aluminum · 0.8 mm zinc
Mechanism housing datum tolerance
±0.05 mm bore to mounting face
Investment casting
10 g to 50 kg · ±0.13 mm on the first 25 mm
Radiator panel width
100 mm to 400 mm
Radiator panel length
up to 3.5 m
Radiator panel straightness
0.5 mm/m precision · 1.3 mm/m standard
Extruded profile
up to 300 mm circumscribing circle
Extrusion wall, minimum
1.2 mm on 6063 · 1.5 mm on 6005A
Annual volume
250 to 250,000 pieces per part number
QUALITY

How We Prove It Before It Ships

Every number on the drawing has to be measured by someone, somewhere. We do it in the supplier’s plant, on the parts that ship — not on your dock, and not on a first article that was made under conditions the production run will never see.

Material certification
Per heat lot · heat number on the part or packaging
NDT
Magnetic particle or ultrasonic per lot on lifting hardware
Hardness
Per heat lot on the certificate, not a blanket statement
Galvanizing
ASTM A123 · 85 µm minimum coating thickness
Pressure test, relief valve bodies
1.5× crack pressure · 100% of parts · at source
Leak test method
Air-under-water or pressure decay · 30 second hold
Porosity
ASTM E505 Level 2 maximum in sealing and load-bearing areas
Gating review
Before the first shot, not after the first return
First article
100% of features, AS9102 format
Production
5 pieces per lot on critical features · CMM at source
Documentation
PPAP Level 3 standard · Level 4 available · 10 year retention
Per shipment
CMM report, material cert, NDT and pressure test records
TIMELINE

Lead Times

01
3 to 5
business days
Quote turnaround
02
5
business days
DFM feedback
before tooling · no cost
03
2 to 4
weeks
Prototype, machined
04
10 to 16
weeks
Forging die
05
10 to 18
weeks
Die casting tool
06
6 to 10
weeks
Extrusion die
07
2 to 4
weeks
First article inspection
from tool approval
08
8 to 12
weeks
Production, tooled part
09
2 to 5
days
From stock
from Columbus, Monterrey or Poland
COMPONENTS

Components We Engineer & Deliver

Three assemblies. All five MES processes appear in a single medium-voltage cabinet.

Pad-Mount & Distribution Transformer

75 to 2,500 kVA. Six to twelve bushing wells, one relief valve, four lifting lugs and up to twenty radiator sections per unit.

Bushing well and terminal stud — machined C11000 or C36000 — Ø25 to 75 mm, tin 8 to 20 µm
Pressure relief valve body — A380 die cast — cracks 10 to 15 psi, tested to 1.5× at source
Lifting lugs — forged A668 Cl.D or 1045, galvanized to ASTM A123, 4:1 design factor
Radiator fin panels — 6063-T5 extrusion to 3.5 m, straightened 0.5 mm/m
Tap changer shaft — forged 304 or 316, Ø12 to 25 mm, straightness 0.1 mm/100 mm
Drain and fill valve body — investment cast CF8M or C83600 — 1 to 2 in NPT
Cabinet hinges, latches and pentahead lock — Zamak 3 or 5, 10,000 cycle rated
Ground pad — forged and machined C11000, UL 467, 95% IACS minimum

Power Transformer

Same families, larger, with tighter documentation. Load-bearing forgings MT or UT inspected and certified per heat lot.

Bushing turret flange — machined from plate to Ø1,200 mm — 0.10 mm flatness, 1.6 µm Ra
Jacking and lifting lugs — forged to 12 kg, MT or UT inspected, 4:1 design factor
Oil valve bodies and sampling ports — investment cast and machined
Machined copper lead clamps — C11000, plated at the contact face
Conservator tank fittings — cast and machined
Buchholz and relay housings — A380 die cast, 1.5 mm minimum wall
Cooling fan brackets and shrouds — die cast and stamped
Structural base and skid framing — 6005A extrusion, machined

Medium-Voltage Switchgear

5 to 38 kV. The assembly where all five MES processes appear inside one cabinet.

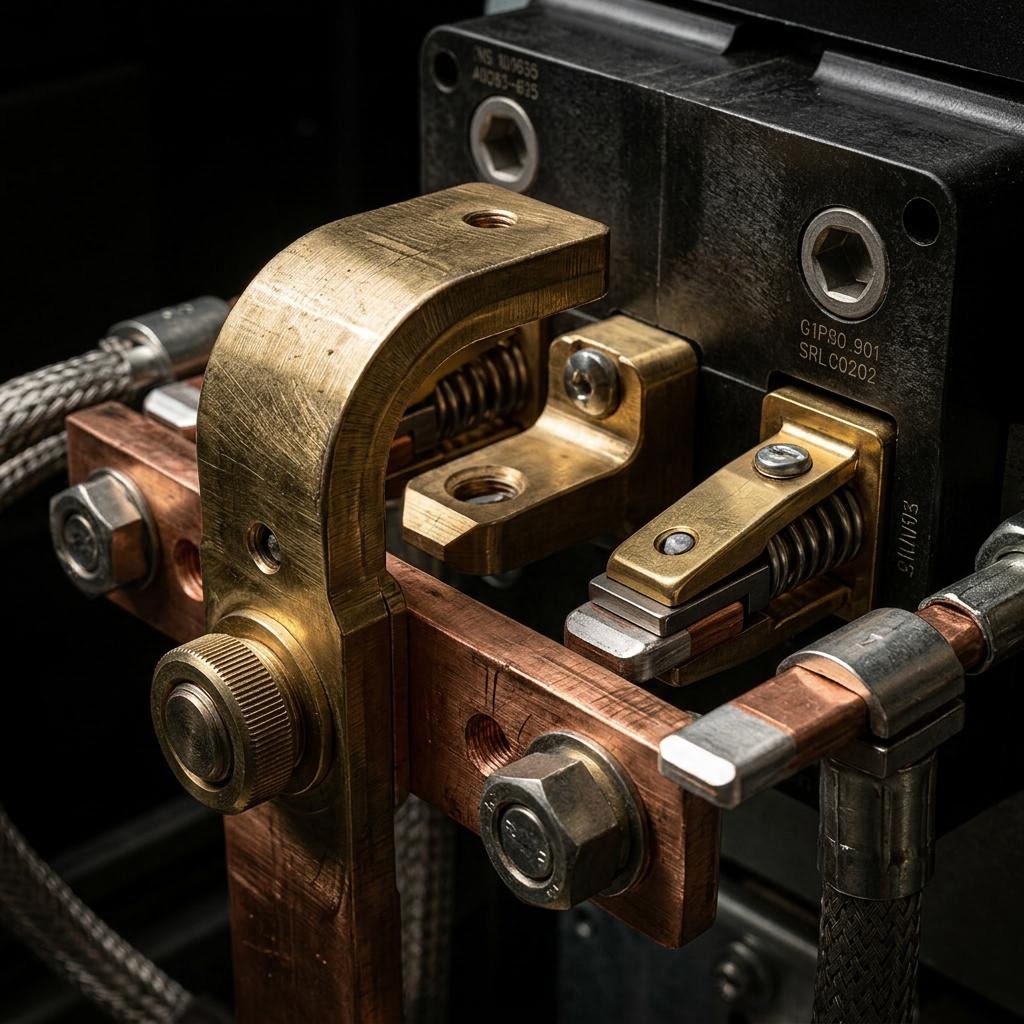
Operating mechanism housing — A380 die cast — ±0.05 mm bore to mounting face, 10,000 operations
Trip latch and contact carrier — investment cast 17-4PH H900 — ±0.13 mm first 25 mm
Operating shaft — forged 4140 Q&T, Ø20 to 60 mm to 900 mm, straightness 0.1 mm/100 mm
Primary bus and bus stabs — machined C11000, plated at the contact face
Breaker cradle and truck frame — 6005A extrusion, machined
Enclosure framing and panels — 6063 and 6005A extrusion, 1.2 mm minimum wall
Cable entry and gland plates — machined aluminum
Also: racking screws, shutter components, arc chute frames, insulator brackets, instrument transformer mounts, door hardware, louvers, control enclosures. Vacuum interrupters, relays and CTs OEM-supplied.
ENGINEERING

What Engineers Ask Us

Five specifications decide whether this hardware performs for thirty years. All five are set on the drawing.

Closed: Plated is not a specification.

Open: A bushing stud carries current in a cabinet that breathes moisture for thirty years. Tin at 8 to 20 µm handles corrosion and adds contact resistance. Silver at 5 to 13 µm conducts better and galls under torque if thin. Specify thickness, standard and measurement location — plating on the flat is not plating at the contact face.

Closed: Grain flow follows the part in a forging. It runs in no particular direction in a casting.

Open: On a lifting lug the grain follows the load path from the weld to the hook. Specify forged for anything carrying a rated load, with heat-lot certification and MT or UT per lot. A certificate saying the material meets the standard is a different document from one saying this batch came from this heat.

Closed: A porous casting passes a dimensional check and a visual, then leaks in service.

Open: Specify ASTM E505 Level 2 maximum in sealing areas, pressure test at 1.5× crack pressure with a 30 second hold on 100% of parts, and specify that it happens at source. The fix is usually a gating change rather than scrap — but only if someone is at the machine when the sealing face is cut.

Closed: AA tolerance permits 1.3 mm of bow per meter.

Open: On a 3.5 m radiator panel that is 4.5 mm of deviation — within specification and unusable if the assembly assumed straight. Precision straightening to 0.5 mm/m costs very little when specified before the die is cut, and is expensive or impossible to add afterward.

Closed: The tolerance that matters is between the pivot bores and the mounting face.

Open: A housing correct on every external feature and loose by 0.15 mm between two internal datums passes a first article and changes how the breaker behaves at operation four thousand. Specify the internal stack at ±0.05 mm, separately from the outside profile.

4:1 DESIGN FACTOR — Forged lifting lugs, MT or UT inspected, certified per heat lot.
0.5 MM/M — Precision straightening against a 1.3 mm/m standard.

Forged or Cast for Load-Bearing Hardware?

Both appear on the same transformer. The decision is about how the part is loaded and what has to be provable afterward.

Forged

Grain flow follows the geometry, so strength follows the load path. Roughly 2 to 3 times the fatigue life of an equivalent casting under cyclic load. Certified per heat lot, MT or UT inspectable. More expensive per part, 10 to 16 week die lead time, limited to shapes a die can form.

Cast

Complex geometry in one operation. Investment casting holds ±0.13 mm on the first 25 mm with under 1 mm of machining allowance. Die casting delivers volume at 1.5 mm minimum wall with EMI shielding. Random grain structure, so lower fatigue performance under repeated load.

Forge anything carrying a rated load. Cast anything whose value is in its geometry. On one pad-mount transformer the lifting lugs are forged, the relief valve is die cast, the drain valve is investment cast and the radiator is extruded — sourcing all four from one partner removes four qualification cycles rather than one.

Where We Are Not the Right Answer

The fastest way to be believed about what we can do is to be specific about what we cannot.

Domestic melt and pour. If your specification requires it, a domestic foundry wins and we should not be in the conversation.
Core laminations, windings and bushings. Sourced or supplied by specialty OEMs — not our lane.
ITAR-controlled work and DFARS specialty metal restrictions.
NQA-1 nuclear programs. The qualification burden is real and we do not carry it.
Vacuum interrupters, relays and instrument transformers. OEM-supplied.
Volumes under 250 pieces a year on a hard-tooled part.

Five Processes. One Partner.

01

CNC Machining

Bushing wells, terminal studs, copper bus, turret flanges to Ø1,200 mm. ±0.05 mm general, ±0.013 mm critical, 1.6 µm Ra on gasket faces.

02

High-Pressure Die Casting

Mechanism housings, relief valve bodies, cabinet hardware. 50 to 4,400 tons, 5 g to 40 kg, 1.5 mm minimum wall aluminum, 0.8 mm zinc.

03

Investment Casting

Trip latches, contact carriers, oil valve bodies. 10 g to 50 kg, ±0.13 mm on the first 25 mm, 3.2 µm Ra as-cast.

04

Forging

Lifting and jacking lugs to 12 kg, operating shafts to Ø60 mm and 900 mm. 50 to 4,400 tons, open and closed die, certified per heat lot.

05

Aluminum Extrusion

Radiator panels to 3.5 m, enclosure framing, breaker cradles. To 300 mm circumscribing circle, 1.2 mm minimum wall, straightened 0.5 mm/m.

Materials

C11000 copper and C36000 brass

100% IACS for bus and studs · 95% minimum on UL 467 ground pads · Free-cutting brass where machinability governs

A380 aluminum and Zamak 3/5 zinc

1.5 mm and 0.8 mm minimum wall · EMI shielding · 10,000 cycle cabinet hardware · Zinc is 2.4× the density of aluminum

A668 Cl.D, 1045 and 4140 forging steels

Galvanized to ASTM A123 at 85 µm · 4:1 design factor · 4140 Q&T for torsional load through 10,000 cycles

17-4PH and CF8M stainless

H900 for trip latches under high-cycle fatigue · CF8M leak-tight against hot oil for the service life

6063 and 6005A aluminum

6063-T5 for radiator sections · 6005A-T6 where framing carries structural load · 1.2 mm minimum wall

SUPPLY CHAIN

Built for Assembly Sequences

Transformer output is gated by technician-hours. An hour lost waiting on a twelve-dollar bracket cannot be recovered next week.

01 Global network

Engineering and quality staff employed in eight countries. 250+ qualified suppliers, 3,000+ audited.

02 Warehousing and JIT

Columbus, Monterrey and Poland. 2 to 5 days to your dock, min-max or consignment.

03 Quality

First article on 100% of features. CMM at source. Heat-lot traceability captured at the mill, retained 10 years.

04 Consolidation

One contact and one planner per account, replacing a dozen supplier relationships for a single unit.

Proof in Production

Real programs, real constraints, and what it took to hold the date.

Eaton: 20+ global locations, one managed inventory program

Eaton operates in more than 170 countries. MES runs a fully managed inventory program across twenty-plus of their facilities.

Acuity Brands: twelve weeks of inventory eliminated

Right component, qualified supplier, tooling dialed in — and twelve weeks of inventory behind it. MES restructured the program and released the working capital.

Precision conductors for Eaton's medium-voltage vacuum circuit breakers

When a sudden manufacturing shutdown hit Eaton’s VCP-W program, MES qualified replacement supply and cleared a backlog of nearly one thousand parts in under eight months — taking annual output from 3,000 units to more than 40,000. High-tonnage aluminum die castings with selective tin and silver plating, nearsourced to a partner in Eaton’s own backyard.

FAQS

FREQUENTLY ASKED QUESTIONS

Let's Build the Hardware Around the Core

Qualifying a second source for bushing hardware, consolidating five supplier relationships into one, or standing up a new plant against a schedule — MES delivers the components and the supply chain to get there faster.

Transformer OEM · Switchgear OEM · Data Center OEM · Utility Supplier · EPC and Integrator

Speak to an Engineer